
Upgrading liquid purification systems for enhanced environmental efficiency remains a priority for today’s municipal and industrial facilities. The choice of polymer chemistry plays a key role in ensuring the long-term dependability of large-scale treatment operations. A PAN ultrafiltration membrane integrated into the pretreatment stage offers robust removal of suspended solids and pathogenic organisms. Many facilities have adopted these advanced material solutions to support consistent performance across a variety of treatment applications.
Material Properties and Structural Stability
Modified polymer chemistry yields exceptional mechanical strength and thermal stability during continuous high-volume liquid processing tasks. Scientific researchers continuously refine polymer matrices to enhance permanent hydrophilicity and resistance against thermal degradation. A standard PAN ultrafiltration membrane delivers outstanding separation performance while withstanding demanding chemical cleaning interventions. Proper material engineering prevents premature fiber snapping and maintains consistent permeability standards over extended operating hours.
Specialized structural modifications successfully address historical anti-pollution shortcomings associated with standard polymer formulations. Technical enhancements optimize pore distribution networks to prevent sudden transmembrane pressure spikes during heavy particulate loads. Plant engineers rely on these structural improvements to maintain stable flux rates without frequent maintenance downtime.
Mechanics of Inside-Out Hollow Fiber Filtration
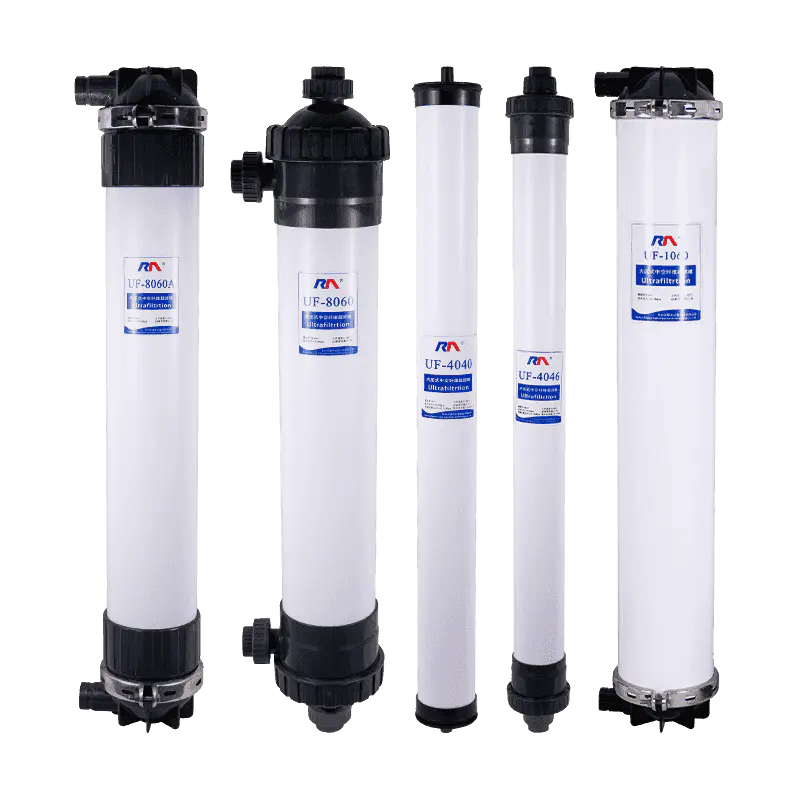
External pressure configurations distribute incoming raw fluid efficiently across massive active membrane filtration surface areas. Liquid flows inward through microscopic pores, leaving suspended colloids and microscopic pathogens trapped outside the hollow fibers. Runmo inside-out ultra filtration membrane elements utilize this reliable hydrodynamic design to prevent internal particulate clogging. Effective cross-flow fluid dynamics sweep accumulated debris away from active surfaces continuously.
Central pipe bracket designs ensure uniform filament distribution and smooth internal fluid flow profiles throughout the module. Reliable physical performance means that routine water washing and chemical cleaning cycles will not compromise structural integrity. Selecting appropriate flow configurations maximizes overall system efficiency and extends component operational lifespans significantly.
Full-Volume Versus Cross-Flow Operating Modes
Selecting appropriate filtration modes depends heavily on raw water quality parameters and specific facility processing goals. Full-volume filtration offers significant advantages in energy conservation and high water utilization rates for cleaner feed streams. Conversely, cross-flow filtration discharges accumulated pollutants in real-time, reducing required chemical cleaning frequencies substantially.
Optimizing operational modes prevents excessive fouling layer buildup on active separation surfaces during heavy industrial processing. Facility managers evaluate incoming turbidity levels carefully before determining the most cost-effective filtration strategy for their plant. Operational flexibility ensures that purification trains adapt smoothly to fluctuating environmental conditions.
Advantages Over Traditional Filtration Technologies
Conventional sand filters and multi-media beds often require extensive physical footprints and high manual labor intervention. Modern polymeric hollow fiber systems offer high automation capabilities while occupying roughly half the floor space of traditional methods. High filtration accuracy ensures that downstream reverse osmosis units receive consistently conditioned feed water free of foulants.
Unattended automated operations reduce labor overhead while maintaining strict compliance with municipal environmental discharge standards. Facility upgrades utilizing compact membrane technology achieve rapid return on investment through lower chemical and energy consumption. Modern industrial plants benefit immensely from these space-saving, high-efficiency physical separation barriers.
Industrial Applications in Sector Purification
Industrial manufacturing sectors depend on sophisticated separation techniques to prepare high-purity process water for sensitive production lines. A PAN ultrafiltration membrane is widely applied in boiler recharge water preparation, pharmaceutical manufacturing, and food processing plants worldwide. These systems remove natural organic matter and suspended turbidity while preserving beneficial mineral balances where required.
Facility engineers integrate these versatile units into broader multi-stage purification trains to handle challenging feed water compositions. Tailoring separation stages to specific raw water profiles optimizes energy consumption and chemical usage simultaneously. Industrial processors achieve stringent quality benchmarks without incurring excessive operational expenditures.
Pretreatment Functions for Reverse Osmosis Units
Protecting delicate reverse osmosis active layers from particulate fouling remains a primary engineering objective in modern plants. Upstream ultrafiltration barriers capture colloidal silica, organic macromolecules, and microbial cells before they reach high-pressure modules. Deploying a robust PAN ultrafiltration membrane as a pretreatment safeguard extends the operational lifespan of sensitive downstream components.
System designers prioritize reliable pretreatment trains to prevent irreversible scaling and biological degradation in primary desalination loops. Minimizing particulate loading reduces overall chemical cleaning requirements and lowers long-term plant maintenance costs significantly. Integrated multi-stage protection secures continuous high-pressure performance across demanding industrial environments.
Environmental Protection and Resource Recovery
Modern environmental regulations require industrial facilities to minimize wastewater discharge volumes through efficient internal recycling loops. Advanced membrane systems facilitate the concentration and recovery of valuable liquid fractions from complex industrial effluent streams. Processing saline wastewater helps plants comply with strict zero liquid discharge mandates while conserving regional water supplies.
Sustainable liquid management bridges the gap between industrial productivity and ecological conservation on a global scale. Environmental engineers rely on advanced polymer systems to reduce the ecological footprints of large-scale manufacturing operations. Effective recycling initiatives protect natural aquatic ecosystems from harmful chemical and mineral pollutant loads.
Conclusion
As global demand for clean water and efficient resource recovery continues to rise, industrial liquid treatment technologies are advancing rapidly to meet these challenges. Runmo offers a comprehensive portfolio of high-performance filtration solutions engineered for demanding separation tasks across multiple sectors. Specialized components are designed to enhance purification efficiency and support long-term operational sustainability. For tailored municipal or industrial system configurations, facility managers are encouraged to consult the Runmo technical team—expert guidance is available to help optimize plant performance.
